How to Choose the Best CNC Bending Machine in 2026?
Choosing the best CNC bending machine in 2026 requires more than comparing tonnage, price, or a glossy control panel. The right machine must fit your materials, bend lengths, production volume, operator skills, and factory layout. A 100-ton press brake may handle standard steel brackets well, yet struggle with thick stainless-steel panels or repeated high-accuracy work. Small details matter. Back-gauge travel, tooling compatibility, crowning, safety systems, and service response can shape daily output.
Industry data supports a careful, technology-aware decision. Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 92% of surveyed manufacturers viewed smart manufacturing as a major competitiveness driver over the next three years. Connectivity is becoming practical, not decorative. The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023, showing how automation continues to influence production planning. However, a connected factory does not automatically produce better bends. That assumption can fail. Poor programming, unstable material quality, or weak maintenance can still create scrap beside advanced equipment.
This guide examines the evidence behind a modern CNC bending machine purchase. It considers accuracy, cycle time, energy use, automation readiness, total ownership cost, and supplier credibility. Reports from Deloitte and IFR provide useful market context, but they cannot replace measurements from your own workshop. Record actual bend times. Test your most difficult parts. Ask suppliers to demonstrate repeatability with your material and tooling. A machine that looks expensive may reduce labor and rework. A cheaper machine may quietly cost more every month. The best choice is measurable, serviceable, and suitable for the work you truly produce.
Define CNC Bending Requirements: 0.5–25 mm Thickness and 1–6 m Length
How to Choose the Best CNC Bending Machine in 2026?
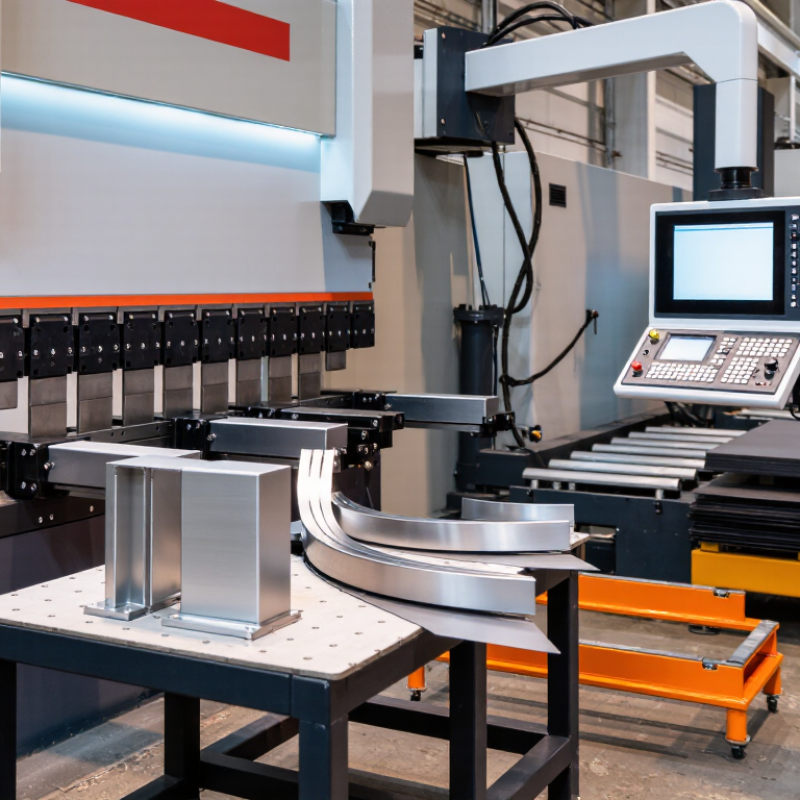
Define your work range before comparing machine specifications. A 0.5 mm sheet needs gentle control and accurate backgauging. A 25 mm plate demands far greater force, rigidity, and tooling strength. These materials should not share one casual calculation. For lengths from 1 to 6 meters, check the effective bending length, not only the machine’s advertised size. A six-meter frame may still struggle with wide plates if its throat depth is limited.
Estimate force using material strength, thickness, bend length, and die opening. Then add a practical reserve. Real workshops face inconsistent batches, surface coatings, and occasional setup mistakes. Machine accuracy also matters. Review repeatability, angle correction, axis control, and calibration records. Ask for test bends using your actual material. A perfect brochure example can still mislead.
Tips: Keep a sample chart for thickness, length, material, die width, and required tonnage. Confirm whether tools support both thin sheets and heavy plates. Inspect the operator interface before purchase; confusing controls create expensive errors. Plan floor space, power supply, loading access, and service response. Do not ignore training. Even advanced automation cannot correct poor setup habits. Recheck your assumptions after the first production trial. That step is often missed.
Match Press-Brake Tonnage to Material: 40–100 Tons per Metre
How to Choose the Best CNC Bending Machine in 2026?
Match Press-Brake Tonnage to Material: 40–100 Tons per Metre
Choosing a CNC bending machine starts with the material, thickness, and bend length. Press-brake capacity is often rated in tons per metre. Mild steel may require about 40–60 tons per metre for common fabrication work. Stainless steel usually needs more force. A practical range is 70–100 tons per metre, depending on its grade and thickness.
Calculate the working load before comparing machine specifications. Multiply the required tons per metre by the actual bend length. A two-metre stainless-steel bend at 80 tons per metre may need approximately 160 tons. Tooling width changes the result. Narrow V-dies increase pressure and can overload the machine. Wider dies reduce force but may produce a larger inside radius.
Check the machine’s rated force, not only its maximum length. A useful safety margin protects the frame, tooling, and hydraulic system. I once estimated a load from thickness alone. The calculation looked acceptable, but the narrow die required noticeably more pressure. That was a useful mistake. Material certificates, grain direction, and bend allowance also affect results. Ask for verified force charts and perform a sample bend with your intended tooling. Repeatability matters too. A strong machine still performs poorly if its backgauge shifts or its control settings are inconsistent.
How to Choose the Best CNC Bending Machine in 2026?
Match Press-Brake Tonnage to Material: 40–100 Tons per Metre
Estimated air-bending force per metre for 4–6 mm sheet using a V-opening equal to six times the material thickness. Values are calculated from representative tensile strengths: aluminium 300 MPa, mild steel 450 MPa, stainless steel 650 MPa, and high-strength steel 700 MPa. Final machine selection should also allow for bend length, tooling, material variation, and a practical safety margin.
Evaluate Automation, Energy Use, and 30–50% Cycle-Time Savings
How to Choose the Best CNC Bending Machine in 2026?
Evaluate Automation, Energy Use, and 30–50% Cycle-Time Savings
Choosing a CNC bending machine should begin with your actual production data. Record setup time, bending strokes, operator handling, and hourly output. Then compare machines against the same part mix. A quoted 30–50% cycle-time reduction is possible in highly repeatable work, but it is not automatic. Material thickness, batch size, and programming quality can change the result.
Automation deserves close inspection. Look for automatic angle correction, tool changing, backgauges, and sensors that detect sheet position. These features reduce repeated measurements and operator movement. They also help maintain consistency across shifts. During a factory trial, measure complete cycles, not only machine motion. Include loading, unloading, inspection, and minor stoppages. Small delays matter.
Energy use requires more than a motor rating. Ask for measured kilowatt-hours per finished part. Servo-driven systems may reduce idle consumption, especially during waiting periods. Automatic sleep modes can help in low-volume production. However, poorly adjusted settings can erase those gains. I have seen impressive test figures weaken after installation because operators bypassed energy-saving modes. That result deserves honest review. Check maintenance access, training requirements, guarding, and service documentation before purchase. A fast machine that stops frequently is not efficient. Reliability remains part of productivity.
How to Choose the Best CNC Bending Machine in 2026? — Evaluate Automation, Energy Use, and 30–50% Cycle-Time Savings
| Machine Configuration |
Typical Working Length |
Typical Press Force |
Suitable Material Thickness |
Automation Level |
Typical Electrical Power Draw |
Estimated Cycle Time per Part |
Cycle-Time Saving vs. Conventional Hydraulic Setup |
Best-Fit Production Profile |
| Standard CNC hydraulic press brake |
2,000–3,100 mm |
800–1,600 kN |
1.5–8 mm mild steel |
Programmable backgauge and angle control; manual loading and tool changes |
12–25 kW during active operation |
45–75 seconds |
Baseline |
Mixed production with moderate batch sizes and a broad range of materials |
| CNC electric-hydraulic press brake |
2,500–4,000 mm |
1,000–2,500 kN |
1.5–10 mm mild steel |
Multi-axis backgauge, automatic crowning, programmable sequencing, assisted tool setup |
8–18 kW during active operation |
32–55 seconds |
Approximately 20–30% |
High-repeatability fabrication with frequent program changes |
| High-speed all-electric press brake |
1,250–3,000 mm |
400–1,600 kN |
0.8–6 mm mild steel |
Automatic axis positioning, fast ram movement, offline programming, tool-setting support |
4–12 kW during active operation |
22–40 seconds |
Approximately 30–45% |
Short-run and high-mix work where rapid setup and low energy use are priorities |
| Automated press brake with robotic loading |
2,000–4,000 mm |
1,000–3,200 kN |
1.5–12 mm mild steel |
Robot loading and unloading, automatic part rotation, tool-change assistance, production monitoring |
10–24 kW for the machine; additional power required by the robot and peripherals |
25–45 seconds |
Approximately 35–50% |
Repeat batches, lights-out production, and labor-constrained operations |
| Dual-machine tandem press brake cell |
4,000–8,000 mm combined |
2,000–6,400 kN combined |
3–16 mm mild steel |
Synchronised CNC control, tandem operation, programmable multi-axis backgauges |
25–55 kW during active operation |
40–80 seconds for large-format parts |
Approximately 30–45% |
Long panels, structural components, transport equipment, and oversized enclosures |
| Automated flexible bending cell |
2,500–4,000 mm |
1,000–2,500 kN |
1–10 mm mild steel |
Robotic material handling, automatic tool management, barcode or MES integration, in-process inspection |
12–28 kW for the complete cell, depending on peripherals |
20–38 seconds |
Approximately 40–50% |
High-mix production requiring unattended operation, traceability, and consistent quality |
Evaluation notes:
Energy figures are indicative operating-load ranges for modern equipment and vary with press force, material, stroke length, duty cycle, standby settings, and auxiliary systems. Cycle-time savings depend on part geometry, number of bends, material handling, tool changes, programming quality, and operator experience. Confirm actual performance using representative parts and a time study before purchase.